


Dismantling of the cylinder block was covered in the article — “Dismantling the cylinder block”.
After dismantling the cylinder block it is necessary to determine whether the cylinder block, crankshaft and piston assembly can be reused.
Checking the cylinder block
The flatness deviation of the mating surface of the cylinder block is permitted to be no more than 0.03 mm. Grinding is not permitted.
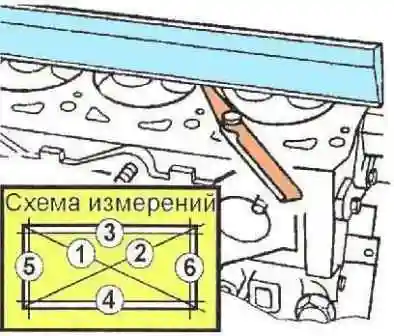
The check must be carried out in accordance with the diagram in Figure 1.
Determining the cylinder diameter
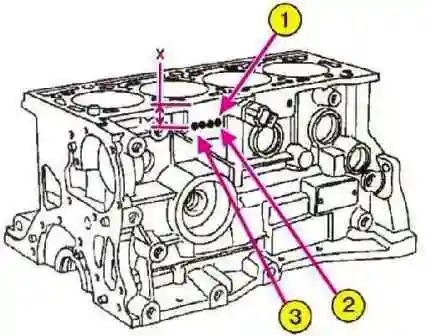
The distance X from the axis of the holes (1) to the mating surface of the cylinder block determines the cylinder diameter group (for more details see the table). Mark (2) corresponds to cylinder No. 1, and mark (3) corresponds to cylinder No. 4 (see Fig. 2).
Before checking, the main bearing caps of the crankshaft must be fitted, with cap No. 1 fitted on the flywheel side.
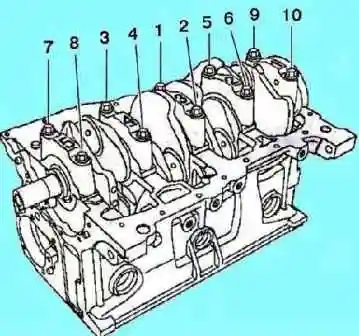
After that we tighten the crankshaft main bearing cap retaining bolts in the sequence shown in Figure 3. We measure the diameters and remove the crankshaft main bearing caps.
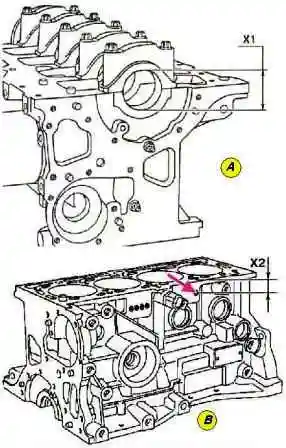
The diameters (X1, Figure 4) of the crankshaft supports are marked by drilling in the area above the oil filter (Fig. 4 (В) according to the arrow). The position (X2) of the holes relative to the mating surface of the cylinder block determines the diameter of the crankshaft supports.
The crankshaft rests in the cylinder block on five supports. The thrust half-rings regulating the axial clearance are fitted on support No. 3.
Permissible crankshaft parameters
- Crankshaft axial play with new thrust half-rings — 0.045–0.252 mm;
- Crankshaft axial play with run-in thrust half-rings — 0.027–0.054 mm;
- Diametral clearance between the crankshaft main journals and the bearings — 0.027–0.054 mm.
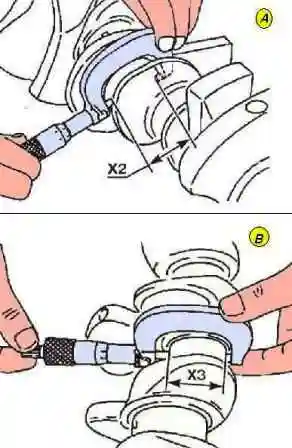
Measurement of the crankshaft journal diameters is shown in Figure 5.
Cylinder diameters

Diameters of the main bearing supports
The dimensions of the diameters of the main bearing supports in the cylinder block are given in Table 2. The dimensions of the main bearing shells are given in Table 3.


Size groups by main journal diameter

Size groups by connecting rod journal diameter

When measuring, the minimum diameter around the journal perimeter is taken as the result.
Crankshaft marking
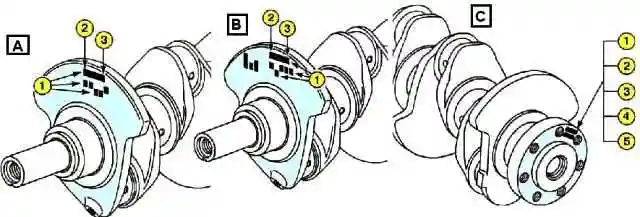
The location of the factory marking and information on the marking are shown in Figure 6.
The marks carry the following information:
- 1 — size groups by main journal diameter;
- 2 — size groups by diameter of main journal No. 1 on the flywheel side;
- 3 — size groups by diameter of main journal No. 5 on the flywheel side;
- 4 — size groups by connecting rod journal diameter;
- 5 — size groups by diameter of connecting rod journal No. 1 on the flywheel side.


