

The valve timing mechanism serves to ensure the intake of a fresh air charge into the cylinders and the exhaust of the burnt gases from them.
The intake and exhaust valves open and close at determined piston positions, which is ensured by the alignment of the marks on the drive gears of the units during their assembly.
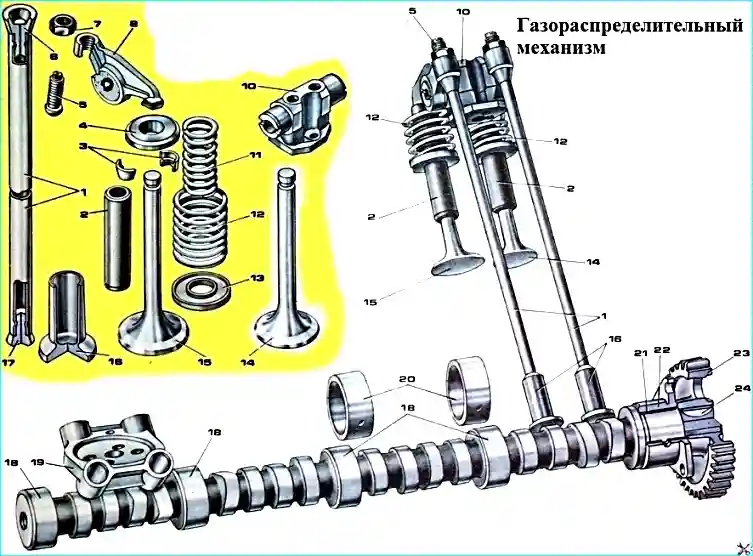
The valve timing mechanism is of the overhead-valve type with a lower camshaft arrangement.
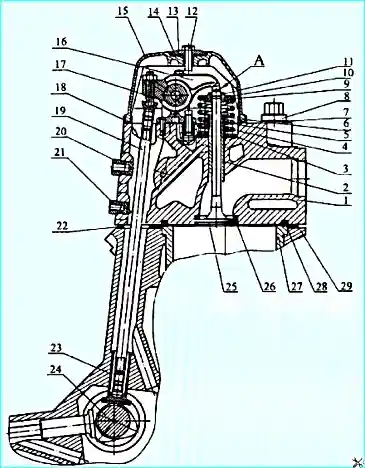
The camshaft cams 24, in accordance with the valve timing phases, actuate the tappets 23.
The pushrods 19 impart an oscillating motion to the rocker arms 16, and these, overcoming the resistance of the springs 4 and 5, open the valves 25.
The valves close under the action of the compression force of the springs.
The camshaft is made of steel; the cams and supporting journals have been high-frequency heat-treated;
it is installed in the centre of the cylinder block on five plain bearings, which are steel bushes cast with antifriction alloy.
The diameter of the bushes is 6 mm larger compared with the bushes of the mod. 740.10 engine.
The camshaft is of increased dimension, with modified valve timing phases and valve lift compared with the camshaft of the mod. 740.10 engine.
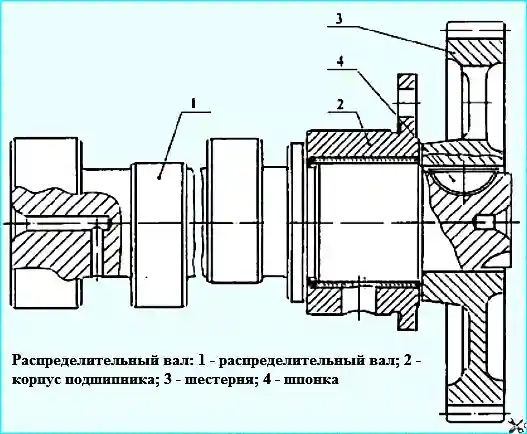
On the rear end of the camshaft a straight-toothed gear 3 is press-fitted.
The camshaft drive is provided from the crankshaft gear through intermediate gears.
The gears are made of steel, stamped with heat-treated teeth.
To ensure the prescribed valve timing phases, the gears are installed during assembly according to the marks stamped on the end faces.
Against axial displacement, the shaft is fixed by the housing 2 of the rear support bearing, which is fastened to the cylinder block by three bolts.
The fitting diameter of the rear support bearing housing is larger compared with the bearing housing of the mod. 740.10 engine.
The installation of the rear support bearing housing of the camshaft of the mod. 740.10 engine is not permissible, as it will lead to a critical drop in the oil pressure in the system and to premature failure of the engine.
The valves are made of heat-resistant steel.
The working chamfer angle of the valves is 90°. The intake valve head diameter is 51.6 mm, the exhaust — 46.6 mm; the intake valve lift height — 14.2 mm, the exhaust — 13.7 mm.
The geometry of the intake and exhaust valve heads ensures the corresponding gas-dynamic parameters of gas intake and exhaust, and therefore their replacement with the valves of the mod. 740.10 engine is not recommended.
The valves move in guide bushes made of cermet.
To prevent oil from entering the cylinder and to reduce its consumption by burning, rubber sealing collars are installed on the valve guides.
The tappets are of the plate type with a profiled guide part, made of steel with subsequent surfacing of the plate surface with chilled cast iron.
The tappet has been subjected to chemical-thermal treatment.
The valve rocker arms are made of steel, stamped, and represent a two-arm lever in which the ratio of the large arm to the small arm is 1.55.
The intake and exhaust valve rocker arms are installed on a common support and fixed in the axial direction by a spring retainer.
The valve rocker arms of the 740.11-240 engine, unlike the rocker arms of the mod. 740.10 engine, have no bronze bush.
The tappet guides are cast integrally with the cylinder block.
The tappet pushrods are made of steel, hollow with press-fitted ends. The pushrods are 3 mm shorter than the pushrods of the mod. 740.10 engine and are not interchangeable with them.
The rocker arm support is made of cast iron, its journals have been subjected to high-frequency heat treatment.
The diameter of the journals is 2 mm larger compared with the journals of the rocker arm support of the mod. 740.10 engine.
The valve springs are helical, two are installed per each valve.
The springs have different winding directions.
The wire diameter of the outer spring is 4.8 mm, of the inner — 3.5 mm. The pre-set force of the springs is 355 N, the total working force — 821 N.
The springs are interchangeable with the springs of the mod. 740.10 engine.
The cylinder heads 1 (Fig. 1) are separate for each cylinder, made of aluminium alloy.
The cylinder head has a cooling cavity communicating with the cooling cavity of the block.
To reinforce the bottom of the head, its thickness in the exhaust channel zone has been increased and an additional rib has been made compared with the cylinder head of the mod. 740.10 engine.
Each cylinder head is installed on two locating pins pressed into the cylinder block and is fastened by four bolts of alloy steel.
One of the locating pins simultaneously serves as a bush for supplying oil for the lubrication of the valve rocker arms.
The bush is sealed by rubber rings.
In the head, compared with the head of the 740.10 engine, the drain hole for the engine oil from under the valve cover into the pushrod cavity has been increased.
The windows of the intake and exhaust channels are located on opposite sides of the cylinder head.
The intake channel has a tangential profile to ensure the optimal rotational movement of the air charge, which determines the parameters of the working process and the environmental performance of the engine, therefore replacement with the cylinder heads of the mod. 740.10 engine is not permitted.
Into the head, cast-iron seats and cermet valve guide bushes are pressed.
The valve seats have an increased interference in the fit compared with the seats of the mod. 740.10 engine and are fixed by a sharp edge.
The exhaust seat and valve are profiled to ensure lower resistance to the exhaust of the burnt gases.
The use of the exhaust valve of mod. 740.10 is not recommended.
The joint «cylinder head — liner» (gas joint) is gasketless (Fig. 4).
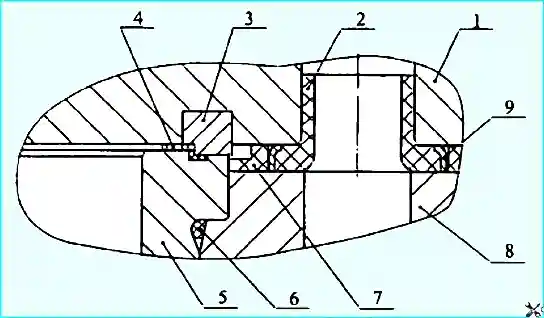
Into the bored groove on the lower plane of the head, a steel sealing ring 3 is pressed. By means of this ring the cylinder head is installed on the collar of the liner.
The tightness of the seal is ensured by the high precision of machining of the mating surfaces of the sealing ring and the cylinder liner 5.
The sealing ring additionally has a lead coating to compensate for the micro-roughness of the surfaces to be sealed.
To reduce the harmful volumes in the gas joint, a fluoroplastic filler gasket 4 is installed.
The filler gasket is fixed on the protruding collar of the gas joint ring by means of a reverse cone with interference.
The use of the filler gasket reduces the specific fuel consumption and the smoke opacity of the exhaust gases. The filler gasket is for single use.
To seal the coolant bypass channels, sealing rings 2 of silicone rubber are installed in the holes of the bottom of the head.
The space between the head and the block, the engine oil drain holes and the pushrod passage holes are sealed by the gasket 7 of the cylinder head made of heat-resistant rubber.
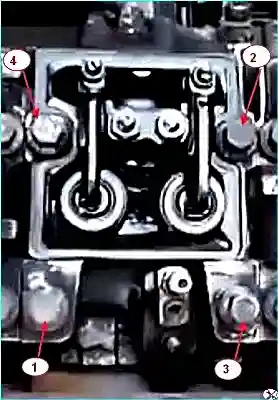
During engine assembly, the cylinder head mounting bolts should be tightened in three stages in the order of increasing numbers indicated in Fig. 5.
The tightening torque values should be:
- 1st stage — up to 39–49 N·m (4–5 kgf·m);
- 2nd stage — up to 98–127 N·m (10–13 kgf·m);
- 3rd stage — up to 186–206 N·m (19–21 kgf·m).
Before screwing in, lubricate the bolt threads with a layer of graphite grease.
After tightening the bolts, it is necessary to adjust the clearances between the valves and the rocker arms.
The valve mechanism is closed by an aluminium cover 15 (see Fig. 1).
For sound insulation and sealing of the joint cover — cylinder head, an anti-vibration washer 14 and a rubber sealing gasket 19 are used.
The cylinder head cover mounting bolts should be tightened to a torque of 12.7–17.6 N·m (1.3–1.8 kgf·m).
Main faults of the valve timing mechanism
Deviations in the operation of the valve timing mechanism during natural wear of the parts cause a deterioration in the dynamics of the mechanism and contribute to accelerated wear of the mating surfaces.
Of the total number of failures of all engine systems, 25–27 % are accounted for by the valve timing gear.
The main engine faults caused by valve timing gear faults may be the following:
- reduction of engine power, increase in fuel and oil consumption;
- increase in the smoke opacity of the exhaust gases;
- reduction of the oil pressure in the engine system at a temperature above 0 °C;
- unstable operation of the engine at idling;
- operation of the engine with misfires or overheating;
- fluid leaks in the connections of the cooling system.
The signs of valve timing gear faults are knocks in the cylinder head.
A ringing knock in the cylinder head is caused by the valves knocking against the rocker arms due to a large thermal clearance between the valve and the nose of the rocker arm.
A dull metallic knock at idling and its intensification when fuel is supplied are a sign of breakage of the valve springs or jamming of the valves.
A loose seating of the valve on its seat occurs in the absence or reduction of the thermal clearance between the nose of the rocker arm and the valve, as well as in case of violation of the load-bearing capacity of the fixed joint cylinder head — valve seat.
In case of loose seating of the valve on its seat, clearances are formed in certain areas between the valve and the seat.
The incandescent gases under pressure and at high speed pass into the gaps formed, therefore the chamfer surfaces in that place corrode intensively and the fit of the chamfer to the seat deteriorates.
Combustion products accumulate on the chamfer surface, as a result of which the tightness of the joint is violated.
An analysis of the characteristic damages of the valves and their seats shows that about 90 % of all damages occur in case of violation of the tightness of the joint seat — valve.
With an increase in the thermal clearance, the valve lift height decreases, as a result of which the filling and scavenging of the cylinders deteriorate, and the impact loads and wear of the valve timing gear parts increase.
With very small thermal clearances, as a result of burning or wear of the working chamfers of the valve or valve seat, the tightness of the combustion chamber is not ensured, the engine loses compression, overheats and does not develop full power.
The most frequently encountered valve timing gear faults are the following:
- premature wear of the seating surfaces of the seat and the valve; wear of the valve guide bush;
- violation of the stability of the fit in the mating valve seat — cylinder head;
- deformation of the cylinder head;
- deformation of the valve seat and stem;
- deformation of the valve head; breakage of the valve stem and corrosion; wear of the holes for the tappets;
- wear of the camshaft bushes; wear of the camshaft cams; wear of the valve rocker arms.
Before carrying out technical maintenance, individual monitoring of the condition of the valve timing gear is necessary, which makes it possible, with the aid of special equipment and without dismantling the engine, to detect in good time the above-mentioned hidden faults and to determine the list of preventive and repair actions.
The technical condition of the valve timing gear should be assessed by diagnostic parameters, and the necessity of carrying out maintenance and repair operations should be determined by the limit values of these parameters.
A characteristic defect of the pushrods: loosening of the seating of the ends and bending of the pushrod stem.
The characteristic defects of the valves are wear of the working chamfers, bending of the stem, breakage of the valve head, wear of the valve end.
The characteristic defects of the tappets are wear of the plate, pitting on the working surface, wear of the stem.
Worn plates and tappet stems are restored by chrome plating.
After restoration, the valves are lapped into the seats of the cylinder heads.


