


We covered engine dismantling in the article «Engine dismantling».
In this article we consider the inspection of the parts and the preparation of the main parts for assembly: cylinder block, pistons with rings, crankshaft, shells, thrust half-rings and flywheel.
Cylinder block
The cylinder block of the VAZ-2112 engine also bears the number «21083», as do those of the 2110 and 2111 engines, but they are not interchangeable: the holes for the cylinder head bolts have an M10×1.25 thread (unlike M12×1.25 for the blocks of the 2110 and 2111 engines) and a smaller depth.
Another difference is due to the more severe thermal regime of the 2112 engine compared with the 2110 and 2111 engines. To cool the pistons during engine operation, their crowns are washed from below with oil through special jets pressed into the second, third, fourth and fifth main bearing supports.
The cylinders are bored directly in the block. The nominal diameter of 82 mm can be increased during repair by 0.4 or 0.8 mm.
The cylinder class is marked on the lower face of the block with Latin letters corresponding to the cylinder diameter in mm: А — 82.00–82.01, В — 82.01–82.02, С — 82.02–82.03, D — 82.03–82.04, Е — 82.04–82.05.
The maximum permissible cylinder wear is 0.15 mm on diameter.
Wash the cylinder block thoroughly and clean the oil galleries. After blowing through and drying with compressed air, inspect the cylinder block. Cracks in the supports or elsewhere in the cylinder block are not permitted.
If coolant ingress into the sump is suspected, check the tightness of the cylinder block on a special test bench. To do this, plug the openings of the cylinder block cooling jacket and pump water at room temperature into it under a pressure of 0.3 MPa (3 kgf/cm²). For two minutes no water leakage from the cylinder block must be observed.
If oil ingress into the coolant is observed, without fully dismantling the engine check whether there are cracks in the cylinder block in the areas of the oil galleries. To do this, drain the coolant from the cooling system, remove the cylinder head, fill the cylinder block cooling jacket with water and supply compressed air to the vertical oil gallery of the cylinder block. If air bubbles appear in the water filling the cooling jacket, replace the cylinder block.
Check the mating face of the cylinder block with the head using a straightedge and a set of feeler gauges. The straightedge is placed along the diagonals of the face and in the middle in the longitudinal and transverse directions. The flatness tolerance is 0.1 mm.
Check whether the cylinder wear exceeds the maximum permissible — 0.15 mm.
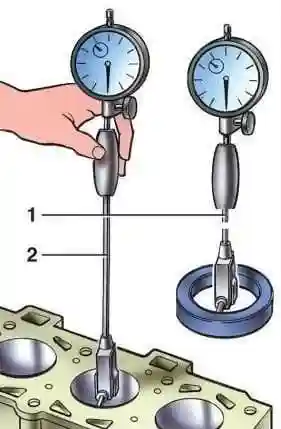
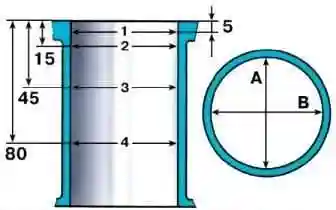
The cylinder diameter is measured with a bore gauge in four bands, both in the longitudinal and transverse directions of the engine. To zero the bore gauge, the 67.8125.9502 calibrator is used. In band 1 the cylinders practically do not wear. Therefore, from the difference of measurements in the first and the other bands one can judge the amount of cylinder wear.
If the maximum wear exceeds 0.15 mm — bore the cylinders to the nearest repair size, leaving an allowance of 0.03 mm on diameter for honing. Then hone the cylinders, maintaining such a diameter that, when the selected repair piston is fitted, the calculated clearance between it and the cylinder is 0.025–0.045 mm.
Piston inspection
Clean the piston of carbon deposits and remove all deposits from the lubrication galleries of the piston and connecting rod. Inspect the parts thoroughly. Cracks of any nature on the piston, piston rings, pin, connecting rod and its cap are not permitted. If there are deep scores on the working surface of the shells, replace the shells with new ones.
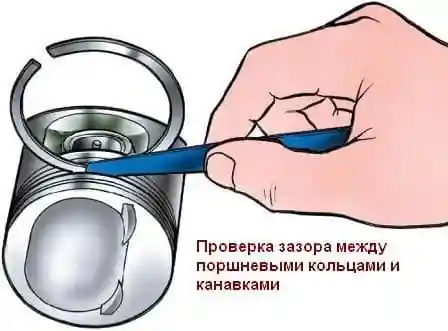
Check the clearance between the piston rings and the grooves with a set of feeler gauges, as shown in the figure, inserting the ring into the corresponding groove. The nominal (calculated) clearance is 0.04–0.075 mm for the upper compression ring, 0.03–0.065 mm for the lower one and 0.02–0.055 mm for the oil scraper ring. The maximum permissible clearances due to wear are 0.15 mm.
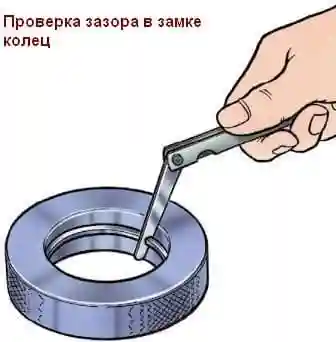
Check the clearance in the piston ring gaps with a set of feeler gauges, inserting the rings into a calibrator whose bore diameter is equal to the nominal ring diameter with a tolerance of ±0.003 mm. For rings of normal size with a diameter of 82 mm, the 67.8125.9502 calibrator can be used. The clearance must be within 0.25–0.45 mm for all new rings. The maximum permissible clearance due to wear is 1 mm.
Crankshaft
The crankshaft of the 2112 engine differs from the crankshaft of the 2110 and 2111 engines in the shape of the counterweights and in increased strength. Therefore, fitting a crankshaft from the 2110 and 2111 engines to the 2112 engine is not permitted.
To supply oil from the main journals to the crankpins, channels are drilled in the crankshaft, the outlet openings of which are closed by pressed-in plugs. On the front end of the crankshaft, on a Woodruff key, a toothed camshaft drive pulley is fitted; the alternator drive pulley is attached to it, which is also a torsional vibration damper of the crankshaft. On the toothed rim of the pulley two teeth out of 60 are missing — the recesses serve for the operation of the crankshaft position sensor.
Inspect the crankshaft. Cracks anywhere on the crankshaft are not permitted. On the surfaces mating with the oil seal lips, scratches, nicks and scores are not permitted.
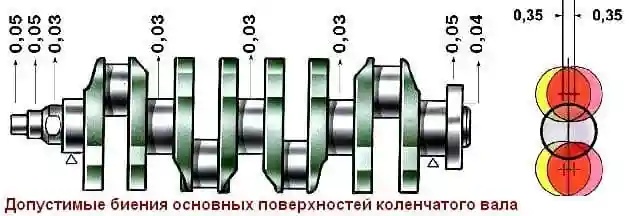
Mount the crankshaft by its end main journals on two prisms and check with a dial gauge the runout of:
- the main journals and the seating surface for the oil pump drive gear (not more than 0.03 mm);
- the seating surface for the flywheel (not more than 0.04 mm);
- the seating surface for the pulleys and the surfaces mating with the oil seals (not more than 0.05 mm).
Measure the diameters of the main and crankpin journals.
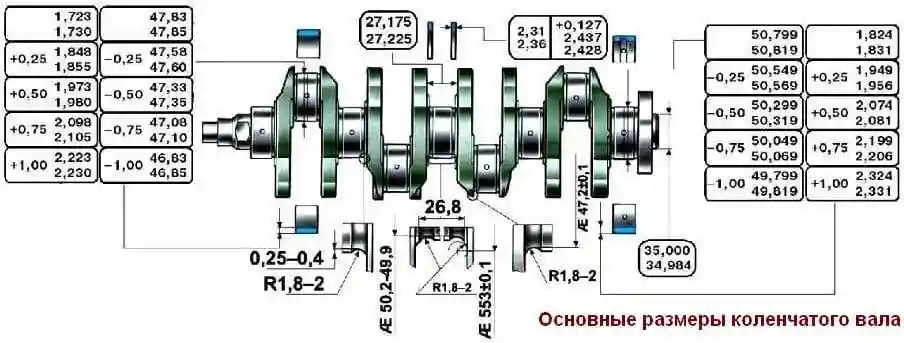
The journals should be ground if their wear is more than 0.03 mm or their ovality is more than 0.03 mm, and also if there are scores and scratches on the journals. Grind the journals reducing the diameter to the nearest repair size. When grinding, maintain the journal fillet dimensions similar to those shown in Fig. 6 for normal crankshaft dimensions.
The ovality and taper of the main and crankpin journals after grinding must be not more than 0.005 mm. The displacement of the crankpin axes from the plane passing through the axes of the crankpin and main journals after grinding must be within ±0.35 mm.
For the check, mount the shaft by its end main journals on prisms and set it so that the axis of the crankpin of the first cylinder lies in the horizontal plane passing through the axes of the main journals. Then use a dial gauge to check the vertical displacement of the crankpins of cylinders 2, 3 and 4 relative to the crankpin of cylinder 1.
After grinding the journals, polish them with diamond paste or GOI paste. After grinding and subsequent finishing of the journals, remove the oil gallery plugs and then machine the plug seats with the А.94016/10 cutter mounted on the А.94016 spindle. Wash the crankshaft and its galleries thoroughly to remove abrasive residues and blow through with compressed air. Using the А.86010 mandrel, press in new plugs and stake each at three points with a centre punch.
On the first crankshaft web, mark the amount of reduction of the main and crankpin journals (for example, К 0.25; Ш 0.50).
Shells
No fitting operations may be performed on the shells. In case of scores, scratches or detachment, replace the shells with new ones.
The clearance between the shells and the crankshaft journals is checked by calculation (after measuring the parts). It is convenient to use calibrated plastic wire to check the clearance. In this case the checking method is as follows:
- thoroughly clean the working surfaces of the shells and of the corresponding journal and place a piece of plastic wire on its surface;
- fit onto the journal the connecting rod with its cap or the main bearing cap (depending on the type of journal being checked) and tighten the nuts or securing bolts. Tighten the connecting rod bolt nuts to a torque of 51 N·m (5.2 kgf·m), and the main bearing cap securing bolts to a torque of 80.4 N·m (8.2 kgf·m);
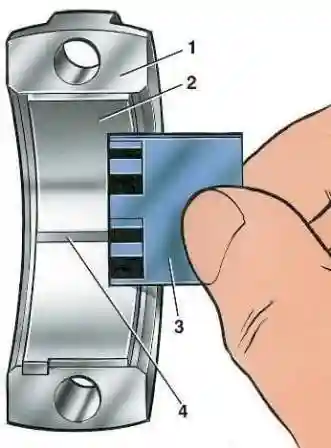
- remove the cap and, from the scale printed on the packaging, determine the clearance value from the flattening of the wire.
The nominal calculated clearance is 0.02–0.07 mm for the crankpin journals and 0.026–0.073 mm for the main journals. If the clearance is less than the limit (0.1 mm for crankpin journals and 0.15 mm for main journals), these shells can be reused. If the clearance is greater than the limit, replace the shells on these journals with new ones. If the crankshaft journals are worn and ground to the repair size, replace the shells with repair ones (of increased thickness).
Thrust half-rings
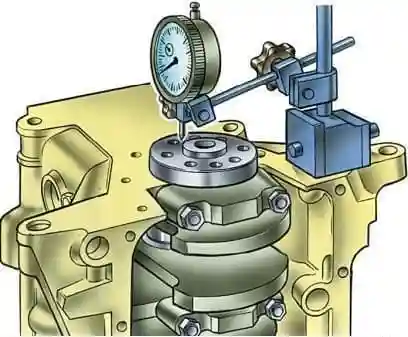
Just as with the shells, no fitting operations may be performed on the half-rings. In case of scores, scratches or detachment, replace the half-rings with new ones. The half-rings are also replaced if the crankshaft end play exceeds the maximum permissible — 0.35 mm. Select new half-rings of nominal thickness or increased by 0.127 mm so as to obtain an end play within 0.06–0.26 mm.
Check the crankshaft free end play. To do this, turn the cylinder block with its rear side upwards and mount on it a stand with a dial gauge so that the gauge probe rests against the crankshaft flange. Moving the shaft up and down (for example, with screwdrivers), measure with the gauge the free end play of the shaft.
Flywheel
Check the condition of the toothed rim and, in case of tooth damage, replace the flywheel.
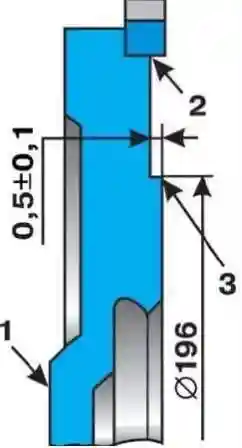
If the flywheel shows temper colours on surface 3, the tightness of the rim on the flywheel must be checked. The rim must not turn at a torque of 590 N·m (60 kgf·m) or move axially under a force of 3.9 kN (400 kgf).
On surface 1 of the flywheel, adjoining the crankshaft flange, and on surface 3 under the clutch driven disc, scratches and scores are not permitted. The flatness tolerance of surface 3 is 0.06 mm. Remove scratches and scores on surface 3 by turning, removing a metal layer not more than 1 mm thick. At the same time, also turn surface 2, without affecting the toothed rim and maintaining the dimension (0.5 ± 0.1) mm. When turning, it is necessary to ensure the parallelism of surfaces 2 and 3 relative to surface 1. The non-parallelism tolerance is 0.1 mm.
Mount the flywheel on a mandrel, centring it by the seating bore with support on surface 1, and check the runout of planes 2 and 3. At the points indicated by arrows in the figure, the gauge must not show runout exceeding 0.1 mm.