


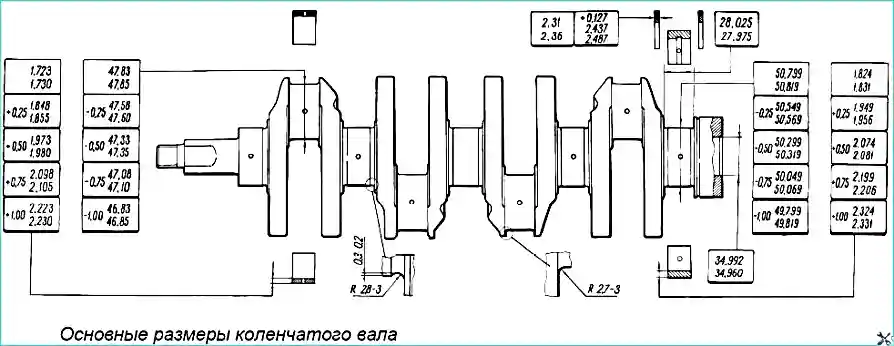
The main dimensions of the crankshaft are given in Figure 1.
The crankshaft is cast, made of cast iron, and five-bearing.
Provision is made for regrinding the crankshaft journals during repair, with a reduction in diameter of 0.25; 0.5; 0.75 and 1 mm.
The axial movement of the crankshaft is limited by two thrust half-rings. They are inserted into the cylinder block seats on either side of the centre main bearing, with a metal-ceramic half-ring (yellow) fitted on the rear side and a steel-aluminium one on the front side. The half-rings are manufactured in two sizes — normal and increased in thickness by 0.127 mm.
The crankshaft bearing shells are thin-walled, steel-aluminium. The upper shells of bearings 1, 2, 4 and 5 of the crankshaft have a groove on the inner surface, while the lower shells have no groove. The shells of the 3rd bearing (upper and lower) have no groove. The big-end bearing shells (upper and lower) also have no groove.
Repair shells are manufactured with increased thickness for crankshaft journals reduced by 0.25; 0.5; 0.75 and 1 mm.
The flywheel is cast, made of cast iron, with a pressed-on steel ring gear for starting the engine by the starter motor. The flywheel is centred by the front bearing of the gearbox input shaft, pressed into the crankshaft. On the rear face of the flywheel, near the ring gear, there is a timing mark in the form of a conical recess. It must be opposite the big-end journal of the fourth cylinder.
Checking the technical condition and repair
Crankshaft
Inspect the crankshaft. Cracks anywhere on the crankshaft are not permitted. On the surfaces mating with the working edges of the oil seals, scratches, dents and scores are not permitted.
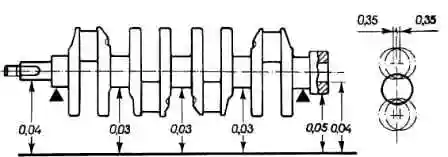
Mount the crankshaft by its end main journals on two vee blocks (Figure 2) and check the runout with a dial gauge:
- of the main journals (not more than 0.03 mm);
- of the seating surfaces for the sprocket and the gearbox input shaft bearing (not more than 0.04 mm);
- of the surface mating with the oil seal (not more than 0.05 mm).
Measure the diameters of the main and big-end journals. The journals should be ground if their wear is more than 0.03 mm or the out-of-roundness of the journals is more than 0.03 mm, and also if there are scores and scratches on the journals. Grind the journals with a reduction in diameter to the nearest repair size (see Figure 1).
When grinding, maintain the fillet dimensions of the journals similar to those given in Figure 1 for normal crankshaft dimensions. The out-of-roundness and taper of the main and big-end journals after grinding must be not more than 0.005 mm.
The offset of the axes of the big-end journals from the plane passing through the axes of the big-end and main journals after grinding must be within 0.35 mm (see Figure 2). To check, mount the shaft by its end main journals on vee blocks and set it so that the axis of the big-end journal of the first cylinder is in the horizontal plane passing through the axes of the main journals. Then check with a dial gauge the vertical offset of the big-end journals of cylinders 2, 3 and 4 relative to the big-end journal of the 1st cylinder.
After grinding the journals, polish them with diamond paste or GOI paste. After grinding and subsequent finishing of the journals, remove the oil gallery plugs and then machine the plug seats with cutter A.94016/10 fitted on spindle A.94016. Thoroughly wash the crankshaft and its galleries to remove abrasive residues and blow them through with compressed air. Using drift A.86010, press in new plugs and stake each one at three points with a centre punch.
On the first web of the crankshaft, mark the amount by which the main and big-end journals have been reduced (for example, K 0.25; Ш 0.50).
Bearing shells
No fitting operations may be carried out on the bearing shells. In the event of scores, scratches or detachment, replace the shells with new ones.
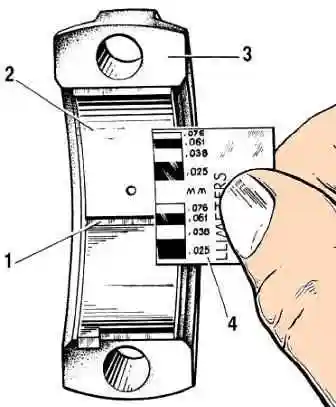
The clearance between the shells and the crankshaft journals is checked by calculation (by measuring the parts). It is convenient to use calibrated plastic wire to check the clearance. In this case, the checking method is as follows:
- thoroughly clean the working surfaces of the shells and the corresponding journal and place a piece of plastic wire on its surface;
- fit the connecting rod with its cap or the main bearing cap (depending on the type of journal being checked) onto the journal and tighten the mounting nuts or bolts.
Tighten the connecting rod bolt nuts to a torque of 51 N·m (5.2 kgf·m), and the main bearing cap mounting bolts to a torque of 80.4 N·m (8.2 kgf·m);
- remove the cap and, using the scale printed on the packaging, determine the clearance from the flattening of the wire (Fig. 3).
The nominal calculated clearance is 0.02—0.07 mm for big-end journals and 0.026—0.073 mm for main journals. If the clearance is less than the limit (0.1 mm for big-end journals and 0.15 mm for main journals), these shells can be reused. If the clearance is greater than the limit, replace the shells on these journals with new ones. If the crankshaft journals are worn and are ground to the repair size, replace the shells with repair shells (of increased thickness).
Thrust half-rings
As with the bearing shells, no fitting operations may be carried out on the half-rings. In the event of scores, scratches or detachment, replace the half-rings with new ones. The half-rings are also replaced if the crankshaft end clearance exceeds the maximum permissible value of 0.35 mm. Select new half-rings of nominal thickness or increased by 0.127 mm so as to obtain an end clearance within 0.06—0.26 mm.
The crankshaft end clearance is checked with a dial gauge, as described in the article “Engine assembly”. The crankshaft end clearance can also be checked on the engine installed in the vehicle. In this case, the axial movement of the crankshaft is produced by pressing and releasing the clutch pedal, and the clearance is determined from the movement of the front end of the crankshaft.
Flywheel
Check the condition of the ring gear and, if the teeth are damaged, replace the flywheel. If the flywheel has temper colours on surface 3 (Fig. 4), the fit of the ring gear on the flywheel must be checked. The ring gear must not turn at a torque of 590 N·m (60 kgf·m).
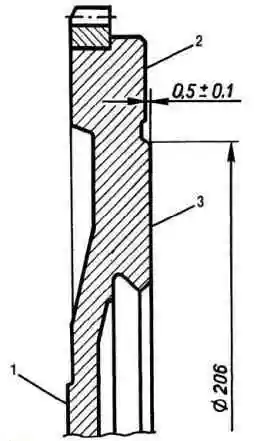
On surface 1 of the flywheel, adjacent to the crankshaft flange, and on surface 3 under the clutch driven plate, scratches and scores are not permitted. Scratches and scores on surface 3 are removed by turning, removing a layer of metal not more than 1 mm thick. At the same time, also turn surface 2, maintaining the dimension (0.5±0.1) mm. When turning, it is necessary to ensure that surfaces 2 and 3 are parallel to surface 1. Tolerance of non-parallelism 0.1 mm.
- Mount the flywheel on a drift, centring it by the seating hole with support on surface 1, and check the runout of planes 2 and 3.
- At the extreme points, the dial gauge must not show runout exceeding 0.1 mm.