


Two compression rings and one oil scraper ring are fitted to the piston.
The compression rings are intended to prevent blow-by of gases into the crankcase during compression and expansion.
In addition, they serve to transfer heat from the piston to the cylinder.
The oil scraper ring serves to remove excess oil from the working surface of the cylinder and to prevent it from entering the combustion chamber.
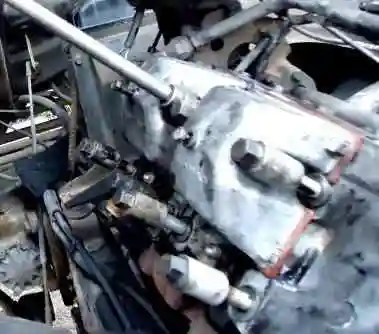
We unscrew the four head retaining bolts (Fig. 1) and remove the cylinder heads.
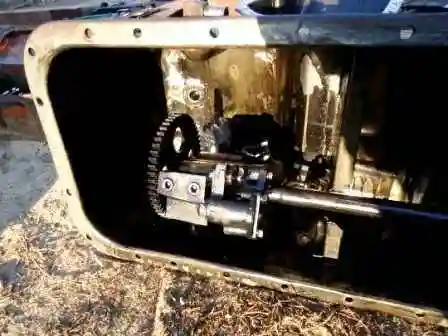
With a 13 mm socket we unscrew the oil sump nuts, remove the engine sump and the sump gasket. If the sump is “stuck”, tap it through a wooden pad.
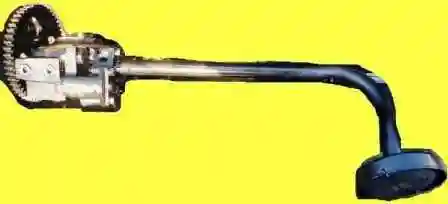
Using 13 and 17 mm spanners, we remove the oil pump.
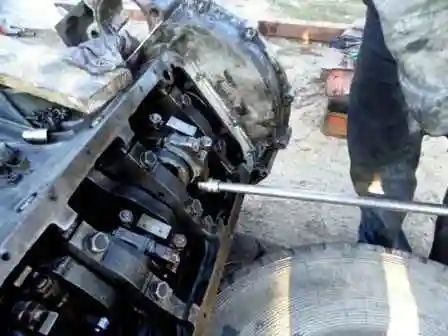
- Unscrew the connecting rod bolt nuts and remove the connecting rod caps (Fig. 4). As the cap is a tight fit, release it with light hammer taps.
- Remove the connecting rod bearing shell from the cap.
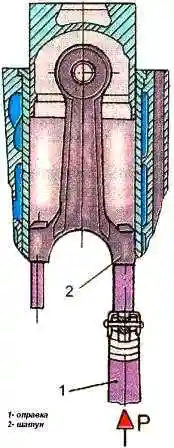
- We push the piston into the cylinder so that it emerges from the cylinder, and then withdraw it together with the connecting rod.
- We remove the connecting rod bearing shell from the rod.
Caution! The piston with the connecting rod must be withdrawn from the cylinder carefully so as not to damage the cylinder bore.
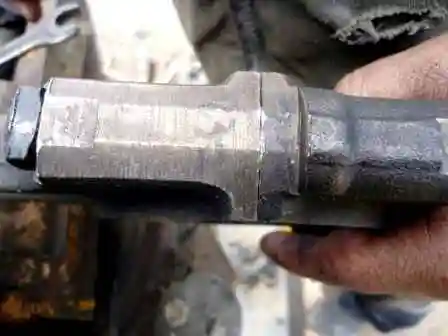
- Check the marks on the connecting rod and the rod cap. If the marks are not visible, mark the rod and cap with the cylinder number.
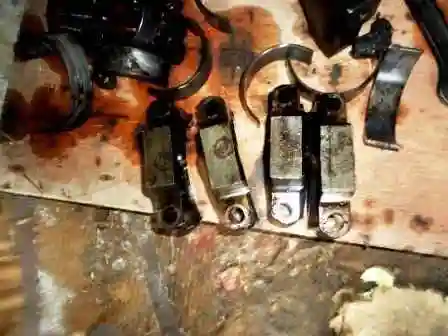
- In the same way we withdraw the remaining pistons with connecting rods.
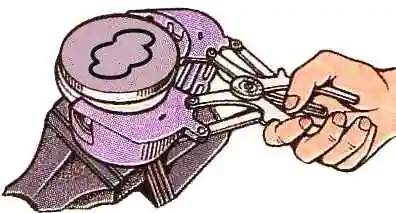
- Using a plunger-type ring expander, we remove the piston rings.
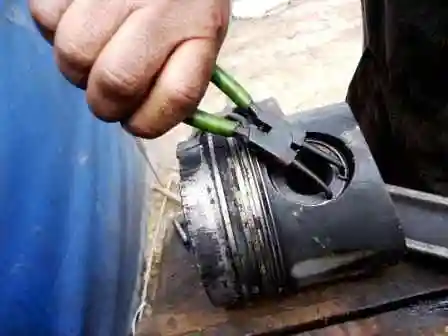
- We remove the circlips from both sides of the piston.
- We heat the piston in an oil bath and withdraw the piston pin from the connecting rod, having first noted the position of the rod relative to the piston.
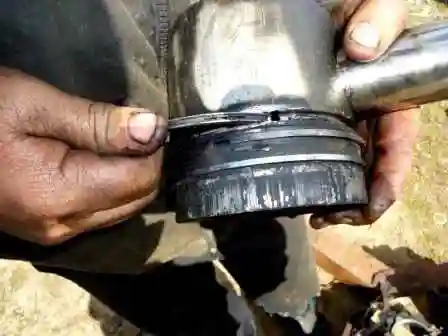
- In the same way, remove the remaining pistons from the connecting rods.
- After dismantling, wash all parts in petrol.
- Clean the pistons of carbon deposits.
- Clean the piston ring grooves with an old piston ring or a fragment of a ring.
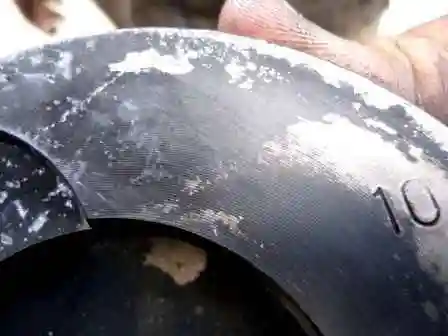
To reduce the clearance above the piston during engine assembly, by selecting the piston version, its protrusion above the sealing end face of the liner is ensured to be 0.5–0.7 mm. The piston version index (10, 20, 30, 40) is marked on its crown and also on the non-working end face of the liner flange.
The diameter of the piston ring in the free state is greater than the cylinder diameter, so when fitted it is pressed firmly against the cylinder walls. In the piston groove the ring forms a labyrinth seal with a small clearance. The gases entering this labyrinth from the space above the piston reduce their pressure and velocity and press the ring against the cylinder wall. The cut in the ring is called the gap. In the working state there must always be a gap at the ring joint so that the ring does not seize when heated. The gap value when fitting the piston into the cylinder is within 0.4–0.8 mm for compression rings and 0.3–0.7 mm for the oil scraper ring. So that the rings can spring freely, they are also fitted in the piston grooves with a small clearance in height. The end clearance of the upper compression ring is somewhat greater than that of the lower one.
The compression rings have a trapezoidal cross-section. The working surface of the upper compression ring is chrome-plated and has a mirror finish; that of the lower one is molybdenum-coated and matt.
During piston movement the rings are pressed either against the upper or the lower faces of the grooves and thereby create the necessary seal preventing blow-by of gases into the crankcase through the grooves. At the same time the compression rings may pump into the combustion chamber the oil they scrape from the cylinder walls: when the piston moves down, the oil collects in the clearance between the ring and the lower face of the groove; when it moves up, the oil is forced into the clearance between the ring and the upper face of the groove. The vacuum in the cylinder during the intake stroke also contributes to this. As the end clearance in the ring — piston groove pair increases, owing to the pumping action of the rings the amount of oil pumped into the combustion chamber grows, as a result of which its consumption rises sharply. Therefore it is necessary to check the end clearance after fitting the rings to the piston.
The oil scraper ring is of composite design; it consists of a cast-iron ring of box section with a chrome-plated working surface and a coiled spring expander. Chrome-plating of the rings increases their wear resistance. The lower groove in the piston for the oil scraper ring has holes all round its circumference to drain the oil scraped by the ring from the cylinder surface.
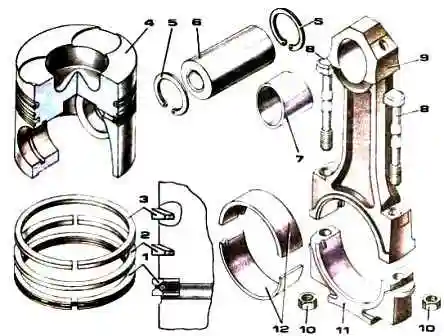
The piston is connected to the connecting rod by a hollow floating-type pin, whose axial movement in the piston is limited by two spring circlips. The connecting rods are steel, of I-section. The lower connecting rod eye is split. For precise seating of the shells, the lower rod eye is finish-machined together with the cap, as a result of which the rod caps are not interchangeable. Pairing marks in the form of three-digit serial numbers are marked on the cap and the rod. In addition, the cylinder serial number is stamped on the rod cap.
The plain bearings in the upper rod eye are bimetallic non-split bushes with a working bronze layer; in the lower rod eye — removable interchangeable shells. The lower rod eye cap is secured by nuts on two bolts pressed into the side lugs of the lower rod eye.
No special locking of the connecting rod bolts and nuts against self-loosening is provided. This is explained by the fact that the connecting rod bolts are automatically protected against self-loosening by friction in the thread, provided the requirements for tightening the connecting rod nut are strictly met. The connecting rod bolts may break due to insufficient or excessive tightening. The bolts must be tightened to an elongation of 0.25–0.27 mm.
Fitting rings, pistons and liners into the 740 KamAZ diesel engine
Fitting the cylinder liners into the block
Before fitting the liners into the block, CIATIM grease is applied to the chamfers. The cylinder liners are inserted by hand force carefully, without allowing the sealing rings protruding from the grooves to be sheared off.
Assembling the connecting rod with the piston
The piston with the pin and connecting rod is assembled after heating the piston to a temperature of 80÷100 °C. The holes in the rod for the pin and the pin itself are pre-lubricated with diesel oil. The pin is fitted by thumb pressure. Pressing the pin in with a tool is not permitted.
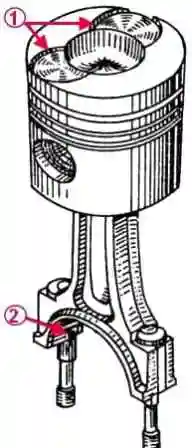
The recesses on the piston and the grooves for the shell tabs on the rod must be located on the same side (Fig. 13). The piston pins are secured by circlips.
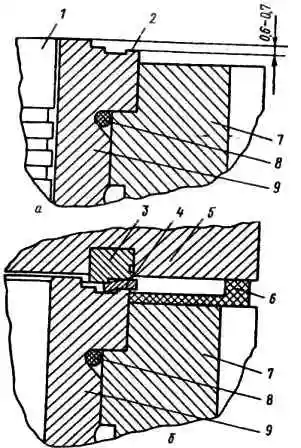
The piston is selected by the distance from the generatrix of the connecting rod journal of the crankshaft in its upper position to the thrust collar of the liner so that the protrusion of the piston crown above the thrust collar of the cylinder liner is within 0.6÷0.7 mm (Fig. 14).
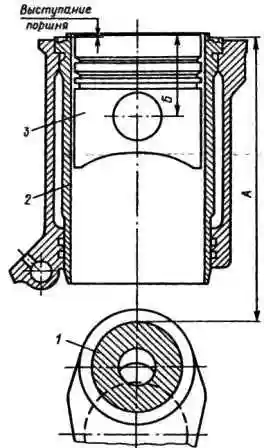
The method of measuring the distance from the generatrix of the connecting rod journal of the crankshaft in its upper position to the sealing collar of the cylinder liner is shown in Figure 15.
Table 1. Data for selecting the piston by the liner
| Piston index | Distance from the generatrix of the connecting rod journal to the thrust collar of the cylinder liner, mm | Distance from the parting plane to the ring centre, mm |
|---|---|---|
| 10 | 260.12–260.24 | 75.67–75.71 |
| 20 | 260.24–260.35 | 75.78–75.82 |
| 30 | 260.35–260.46 | 75.89–75.93 |
| 40 | 260.46–260.57 | 76.00–76.04 |
After the pistons have been selected at the factory, the indices of piston versions 10, 20, 30, 40 are marked on the piston crown and on the non-working protrusion of the liner end face. During assembly, pistons and cylinders with the same index must be selected.
When fitting the piston into the liner, the valve recesses on the piston must be positioned closer to the crankshaft axis. The total clearance between the end faces of the lower rod eyes and the crankshaft journals (axial play) must be at least 0.15 mm.
The piston rings must have thermal clearances before fitting to the piston. The piston ring clearance is measured in a gauge of 120+0.03 mm diameter.
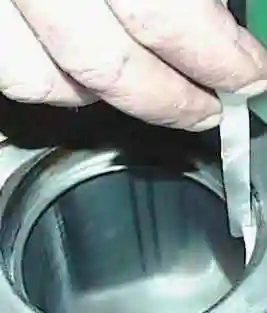
Table 2. Dimensions of piston ring clearances
| Parameters | Clearance after restoration, mm | Permissible clearance, mm |
|---|---|---|
| Ring joint in the compression rings | 0.4–0.6 | 0.8 |
| Ring joint in the oil scraper rings | 0.30–0.45 | 0.7 |
| End clearance of the upper compression ring | 0.12–0.17 | 0.22 |
| End clearance of the lower compression ring | 0.09–0.14 | 0.19 |
| End clearance of the oil scraper ring | 0.07–0.11 | 0.2 |
| Clearance in the piston-liner pair (measured at 0.119–1.162 mm from the piston crown) | 0.12–0.16 | 0.22 |
Fitting the piston rings
- We fit the piston rings using a plunger-type expander (if available).
- The oil scraper ring is inserted into the piston groove and the ring is fitted so that the expander joint is at 180° to the ring joint.
- After that we fit the compression rings. First we insert the molybdenum-coated ring, then the chrome-plated ring.
- The joints of adjacent rings are staggered in different directions.


