


Before reassembly, the cylinder block must be fault-diagnosed and its further service determined.
Dismantling of the engine was covered in the article ‘Dismantling the engine’.
Fault diagnosis of the crankshaft was covered in the article ‘Dismantling and inspection of the crankshaft’.
Repair of the connecting rod and piston group was covered in the article ‘Repair of the CRP’.
- 1. Inspect the block; if there are cracks, replace it.
- 2. Check the tightness of the block water jacket. To do this, plug all openings in the block with wooden plugs except one, to which a compressed air hose is connected.
Immerse the block in a water bath and supply compressed air at a pressure of 1.5 atm.
Air bubbles will emerge at the points of leakage.
Check the tightness of the block oil galleries in the same way.
If leakage is found, the block must be replaced.
3. Inspect the cylinder liners.
If the cylinder bores show scratches, scoring, pitting, etc., bore the liners to the repair size or replace them.
Two repair sizes of liners are provided, as given in the table.
Spare parts include pistons and piston rings of the same repair sizes. All liners must be bored to the repair size, even if defects are found in only one.
4. Check the clearances between the pistons and liners. The nominal clearance should be within 0.024–0.048 mm; the maximum permissible is 0.25 mm.
To ensure the clearance value, pistons and liners are divided by diameter into five size groups: A, B, V, G and D. The letter denoting the liner group is marked on the lower centring part of the liner.
The clearance can be determined by measuring the piston and liner diameters.
The piston diameter is measured in a plane perpendicular to the gudgeon pin axis and 8.0 mm below the pin axis.
The liner diameter is measured in at least three belts within 15–100 mm from the top edge of the liner, in two perpendicular directions.
5. When replacing liners, the new liners are inserted into the cylinder block so that the letter denoting the liner group is located in the transverse plane.
The liner must enter the block completely freely.
A liner fitted with a copper gasket in the block must protrude above the block surface by 0.02–0.1 mm.
The difference in liner protrusion between cylinders must not exceed 0.055 mm (this is ensured by selecting liners by length or by seating them with deformation of the copper gasket).
Before removing the liners from the block, they must be marked so that during reassembly they can be fitted in the same place and in the same position as before dismantling.
When using old liners, the unworn band in the upper part of the liner must be removed flush with the cylinder bore.
6. Check the clearances between the main bearing shells and the crankshaft journals; they should be within 0.02–0.073 mm.
The clearances can be calculated by measuring the diameters of the crankshaft journals and the journal bores with the shells and main bearing caps fitted, or measured using calibrated plastic wire.
The clearances are measured in the following order:
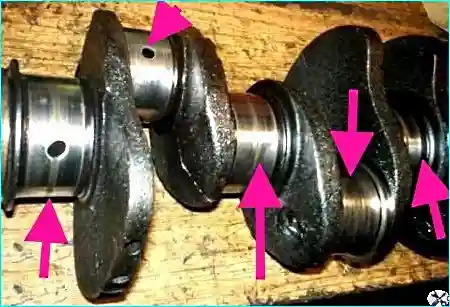
a) Clean the crankshaft journals and bearing shells.
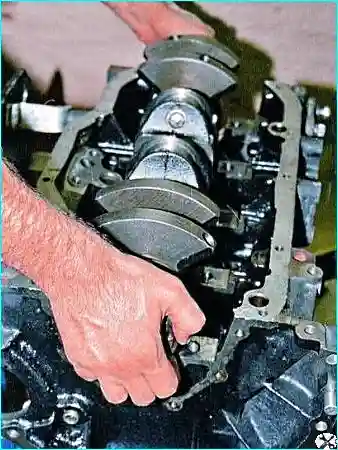
b) Lay the crankshaft on the main bearing saddles with the shells fitted.
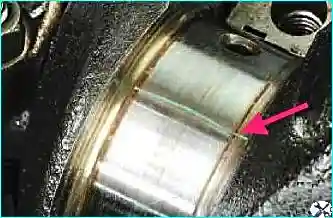
c) Place pieces of calibrated plastic wire on the crankshaft journals.
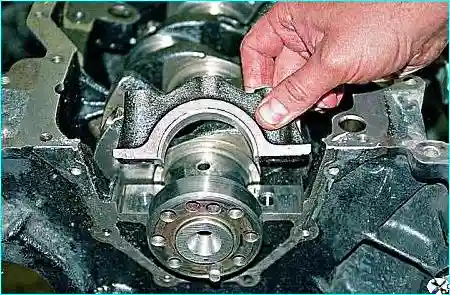
d) Fit the main bearing caps with the shells installed in them.
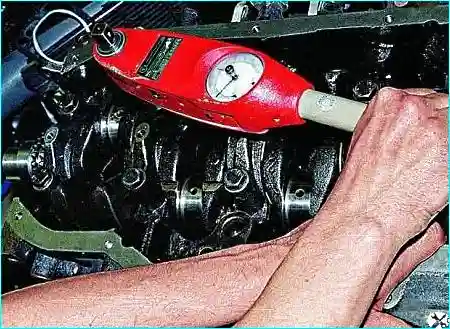
e) Tighten the cap securing bolts to a torque of 100 N·m (10 kgf·m). Turning the crankshaft during this operation is prohibited.
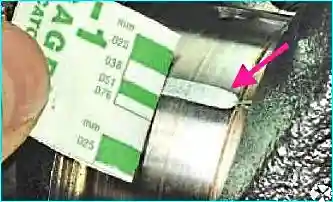
f) Remove the main bearing caps and determine the clearance from the flattening of the wire using the scale printed on the wire packet.
| Group | Nominal size | 1st repair size* | 2nd repair size** | |||
|---|---|---|---|---|---|---|
| Cylinder | Piston | Cylinder | Piston | Cylinder | Piston | |
| A | 92.024–92.036 | 91.988–92.000 | 92.524–92.536 | 92.488–92.500 | 93.024–93.036 | 92.988–93.000 |
| B | 92.036–92.048 | 92.000–92.012 | 92.536–92.548 | 92.500–92.512 | 93.036–93.048 | 93.000–93.012 |
| V | 92.048–92.060 | 92.012–92.024 | 92.548–92.560 | 92.512–92.524 | 93.048–93.060 | 93.012–93.024 |
| G | 92.060–92.072 | 92.024–92.036 | 92.560–92.572 | 92.524–92.536 | 93.060–93.072 | 93.024–93.036 |
| D | 92.072–92.084 | 92.036–92.048 | 92.572–92.584 | 92.536–92.548 | 93.072–93.084 | 93.036–93.048 |
* The 1st repair size is increased by 0.5 mm.
** The 2nd repair size is increased by 1.0 mm.