


The main dimensions of the connecting rod and piston assembly are shown in Figure 1.
The piston is cast aluminium. The mass of the pistons is strictly maintained during manufacture.
Therefore, when assembling the engine, it is not necessary to select pistons of the same mass group.
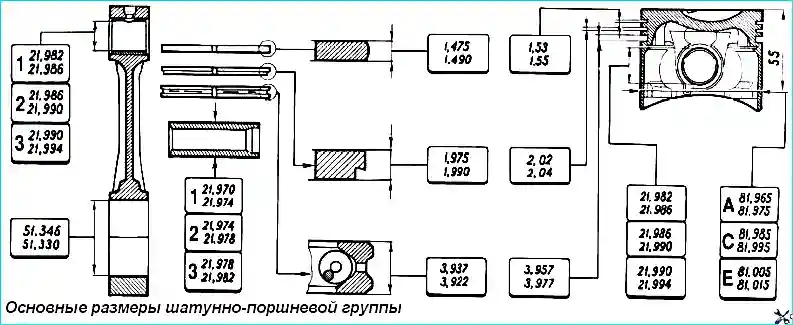
By outside diameter, the pistons are divided into five classes (A, B, C, D, E) at intervals of 0.01 mm. The outer surface of the piston has a complex shape. In height it is barrel-shaped, and in cross-section it is oval. Therefore, the piston diameter must be measured only in the plane perpendicular to the piston pin, at a distance of 55 mm from the piston crown.
By the diameter of the piston pin bore, the pistons are divided into three classes (1, 2, 3) at intervals of 0.004 mm.
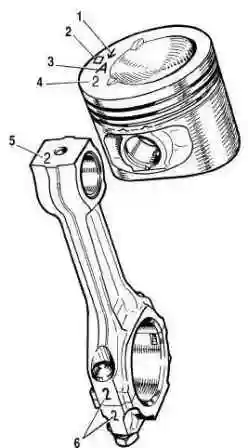
The classes of the piston diameter and of the bore for the piston pin are stamped on the piston crown.
Repair-size pistons are manufactured with an outside diameter increased by 0.4 and 0.8 mm. On the crowns of these pistons a marking is applied in the form of a triangle or a square. The triangle corresponds to an increase in outside diameter of 0.4 mm, and the square to 0.8 mm.
The arrow on the piston crown shows how to orient the piston correctly when fitting it into the cylinder. It must point towards the camshaft drive.
The piston pin is made of steel, hollow, of the floating type, that is, it rotates freely in the piston bosses and the connecting rod bush. The pin is secured in the piston by two steel circlips.
By outside diameter, the pins are divided into three classes at intervals of 0.004 mm. The class is marked with paint on the end of the pin: blue mark — first, green — second, red — third class.
The piston rings are made of cast iron. The upper compression ring has a chrome-plated barrel-shaped outer surface. The lower compression ring is of the scraper type. The oil scraper ring has chrome-plated working edges and an expanding coiled spring (expander).
On repair-size rings a numerical marking “40” or “80” is applied, which corresponds to an increase in outside diameter of 0.4 or 0.8 mm.
The connecting rod is made of steel, forged. The connecting rod is machined together with its cap, and therefore they are not interchangeable separately. To avoid mixing up the caps and connecting rods during assembly, the number 6 (see Figure 2) of the cylinder in which they are fitted is stamped on them. During assembly, the numbers on the connecting rod and the cap must be on the same side.
A steel-bronze bush is pressed into the upper end of the connecting rod. By the diameter of the bore of this bush, the connecting rods are divided into three classes at intervals of 0.004 mm (just like the pistons). The class number 5 is stamped on the upper end of the connecting rod.
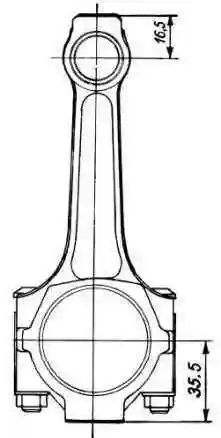
By the mass of the upper and lower ends, the connecting rods are divided into classes (table), marked with paint on the connecting rod shank. Connecting rods of the same mass class must be fitted to the engine. The mass of the connecting rods can be adjusted by removing metal from the bosses on the ends down to the minimum dimensions of 16.5 and 35.5 mm (Figure 3).
Connecting rod classes by mass of the upper and lower ends
| Mass of the connecting rod ends (grammes) | Class | Marking colour | |
|---|---|---|---|
| Upper | Lower | ||
| 186∗2 | 519∗3 | A | white |
| 525∗3 | B | light blue | |
| 531∗3 | C | red | |
| 190∗2 | 519∗3 | D | black |
| 525∗3 | E | violet | |
| 531∗3 | F | green | |
| 194∗2 | 519∗3 | G | yellow |
| 525∗3 | H | brown | |
| 531∗3 | I | orange | |
Since the 2012 production, the masses of the connecting rod ends have changed slightly.
| Mass of the connecting rod ends (grammes) | Class | Marking colour | |
|---|---|---|---|
| Upper | Lower | ||
| 186∗2 | 527∗3 | A | white |
| 533∗3 | B | light blue | |
| 539∗3 | C | red | |
| 190∗2 | 527∗3 | D | black |
| 533∗3 | E | violet | |
| 539∗3 | F | green | |
| 194∗2 | 527∗3 | G | yellow |
| 533∗3 | H | brown | |
| 539∗3 | I | orange | |
Selecting the piston for the cylinder
The calculated minimum clearance between the piston and the cylinder (for new parts) is 0.025—0.045 mm. It is determined as the difference between the minimum cylinder size and the maximum piston size and is ensured by fitting pistons of the same class as the cylinders. The maximum permissible clearance (when the parts are worn) is 0.15 mm.
If, in an engine that has been in service, the clearance exceeds 0.15 mm, the pistons must be reselected for the cylinders so that the clearance is as close as possible to the calculated value.
Pistons of classes A, C and E are supplied as spare parts. This is sufficient for selecting a piston for any cylinder when repairing the engine, since the pistons and cylinders are divided into classes with a slight overlap of sizes. For example, a class C piston may fit cylinders of classes B and D.
Dismantling and reassembly
Dismantling
- Extract the piston pin circlips from the piston, withdraw the pin and separate the connecting rod from the piston.
- Remove the piston rings.
The connecting rod bolts are pressed into the connecting rod. Therefore, in order not to disturb the fit of the bolt in the connecting rod, it is not permitted to press the bolts out of the connecting rods when dismantling the engine and the connecting rod and piston assembly.
If some parts of the connecting rod and piston assembly are undamaged and only slightly worn, they can be reused. Therefore, when dismantling, mark them so that the assembly can subsequently be reassembled with the same parts and fitted into the original engine cylinder.
Reassembly
Before reassembly, select the pin for the piston and connecting rod. On new parts, the class of the pin bores in the connecting rod and piston must be identical to the class of the pin. On parts that have been in service, for correct mating it is necessary that the piston pin, lubricated with engine oil, enters the piston or connecting rod bore under simple thumb pressure (Figure 4) and does not fall out of it if the piston is held as shown in Figure 5.
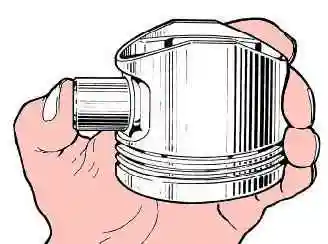
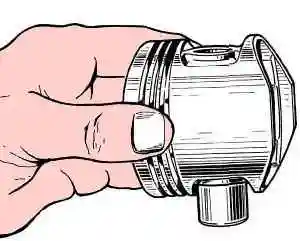
Replace a pin that falls out with another one of the next category. If a third-category pin was inserted into the piston, replace the piston, the pin and the connecting rod.
The connecting rod and piston assembly is reassembled in the reverse order to dismantling. After fitting the piston pin, lubricate it with engine oil through the holes in the piston bosses.
Fit the piston rings in the following order:
- Lubricate the grooves on the piston and the piston rings with engine oil.
- Orient the piston rings so that the gap of the upper compression ring is at an angle of 45° to the piston pin axis, the gap of the lower compression ring is at an angle of approximately 180° to the axis of the gap of the upper compression ring, and the gap of the oil scraper ring is at an angle of approximately 90° to the axis of the gap of the upper compression ring.
- Fit the lower compression ring with the recess downwards (see Figure 1). If the ring bears the mark “Верх” or “TOP”, fit the ring with the mark upwards (towards the piston crown).
- Before fitting the oil scraper ring, check that the joint of the spring expander is on the side opposite the ring gap.
The dismantling and reassembly of the connecting rod and piston assembly can be viewed here.
Checking the technical condition
- Clean carbon deposits from the piston and remove all deposits from the lubrication galleries of the piston and connecting rod.
- Carefully inspect the parts. Cracks of any kind on the piston, piston rings, pin, connecting rod and its cap are not permitted.
- If there are deep scores on the working surface of the bearing shells, replace the shells with new ones.
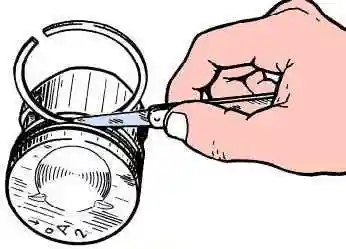
Check the clearance between the piston rings and the grooves with a set of feeler gauges, as shown in Figure 6, inserting the ring into the corresponding groove.
The calculated clearance (rounded to 0.01 mm) for new parts is:
- for the upper compression ring — 0.04—0.07 mm;
- for the lower compression ring — 0.03—0.06 mm;
- for the oil scraper ring — 0.02—0.05 mm.
The maximum permissible clearances when worn are 0.15 mm.
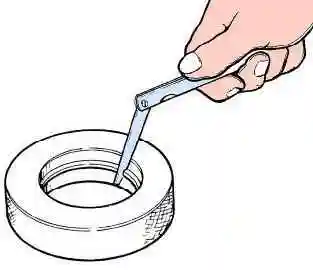
Check the gap in the piston ring end gaps with a set of feeler gauges, inserting the rings into a gauge (Figure 7) whose bore diameter is equal to the nominal diameter of the ring with a tolerance of 0.003 mm. For normal-size rings of 82 mm diameter, gauge 67.8125.9502 may be used.
The gap must be within 0.25—0.45 mm for all new rings. The maximum permissible gap when worn is 1 mm.