


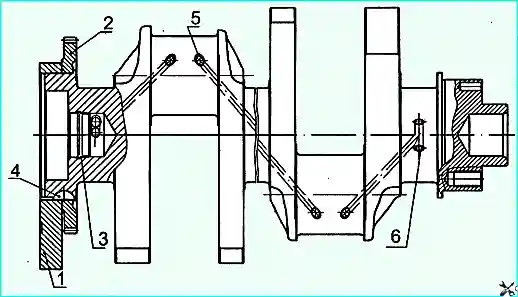
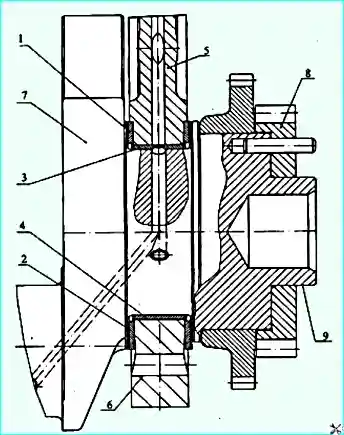
The crankshaft (Figure 1) is made of high-quality steel and has five main journals and four connecting rod journals, connected by webs and mated by transition fillets.
For uniform alternation of the working strokes, the connecting rod journals of the crankshaft are arranged at an angle of 90°.
Two connecting rods are attached to each connecting rod journal (Figure 2) — one for the right-hand and one for the left-hand cylinder bank.
The crankshaft is hardened by nitriding to a depth of 0.5–0.7 mm; the hardness of the hardened layer is not less than 600 HV.
Oil is supplied to the connecting rod journals through the holes in the main journals 8 and the holes 7 (Figure 1).
To balance the inertia forces and reduce vibrations, the crankshaft has six counterweights forged integrally with the crankshaft webs.
In addition to the main counterweights, there is an additional removable counterweight 1, press-fitted onto the shaft; its angular position relative to the crankshaft is determined by the key 5.
To ensure the required imbalance, a recess 6 (Figure 5) is provided on the flywheel.
On the rear end of the crankshaft, a journal 9 (Figure 3) is provided, on which the crankshaft gear 8 and the flywheel 1 (Figure 6) are centred.
On the rear end face of the crankshaft, ten threaded holes M16×1.5-6Н are provided for fastening the crankshaft gear and the flywheel; on the front end face, eight threaded holes M12×1.25-6Н are provided for fastening the torsional vibration damper.
In the cavity of the crankshaft nose, a plug 4 (Figure 1) is installed, through the calibrated hole of which the splined shaft of the front power take-off is lubricated.
Against axial displacements, the crankshaft is fixed by two upper half-rings 1 and two lower half-rings 2 (Figure 3), installed in the grooves of the rear main support of the cylinder block, so that the side with the grooves adjoins the thrust end faces of the shaft.
On the crankshaft nose (Figure 1), the oil pump drive gears 2, 3 and the valve timing mechanism drive gear 8 (Figure 3) are installed.
The crankshaft is sealed by a rubber oil seal 8 (Figure 6), with an additional sealing element — a dust excluder 9. The oil seal is located in the flywheel housing 4.
The oil seal is made of fluoro rubber using the technology of forming the working sealing edge directly in the mould.
Nominal diameters of the crankshaft journals:
- main: 95-0.015 mm;
- connecting rod: 80-0.013 mm.
For engine restoration, eight repair sizes of bearing shells are provided.
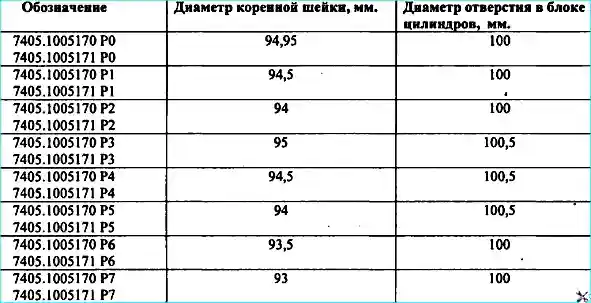
The designation of the crankshaft bearing shells, the diameter of the crankshaft main journals, the diameter of the hole in the cylinder block for these shells are indicated in Table 1.
The designation of the connecting rod lower head shells, the diameter of the crankshaft connecting rod journals, the diameter of the hole in the connecting rod crank head for these shells are indicated in Table 2.
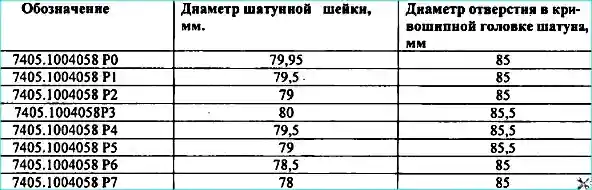
The shells 7405.1005170 Р0, 7405.1005171 Р0, 7405.1005058 Р0 are used in engine restoration without grinding the crankshaft. If necessary, polish the crankshaft journals.
When grinding the crankshaft along the main journals to 94 mm and less, or along the connecting rod journals to 79 mm and less, the crankshaft must be subjected to repeated nitriding.
The tolerance limits for the diameters of the crankshaft journals, the diameter of the hole in the cylinder block and the diameter of the hole in the connecting rod crank head during engine restoration must be the same as for the nominal dimensions.
The crankshaft for the engines 740.50-360 and 740.51-320 has significant differences from the crankshafts of other engine models; these differences make it impossible to use crankshafts of KAMAZ engines of other models.
The marking of the crankshaft, made in the forging on the third counterweight, must be 740.50-1005020.
The main and connecting rod bearings (Figures 2 and 3) are made of steel strip coated with a layer of lead bronze 0.3 mm thick, a layer of lead-tin alloy 0.022 mm thick and a layer of tin 0.003 mm thick.
The upper 3 and lower 4 shells of the main bearings are not interchangeable. In the upper shell there is a hole for oil supply and a groove for its distribution.
Both shells 4 of the connecting rod lower head are interchangeable.
Against turning and lateral displacement, the shells are fixed by protrusions (lugs) entering the grooves provided in the block and connecting rod seats, as well as in the bearing caps.
The shells have design differences aimed at increasing their serviceability during engine boosting by turbocharging; the marking of the shells has been changed to 7405.1004058 (connecting rod), 7405.1005170 and 7405.1005171 (main).
Replacement of the shells during repair with serial ones marked 740 is not recommended, since this will cause a significant reduction in the engine service life.
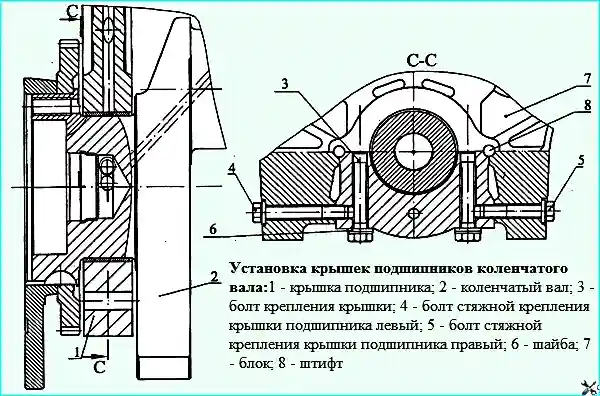
The main bearing caps (Figure 4) are made of high-strength cast iron.
The caps are fastened by means of vertical and horizontal draw bolts 3, 4, 5, which are tightened according to a certain scheme with a regulated torque (see the article Tightening torques of the KAMAZ diesel fasteners).
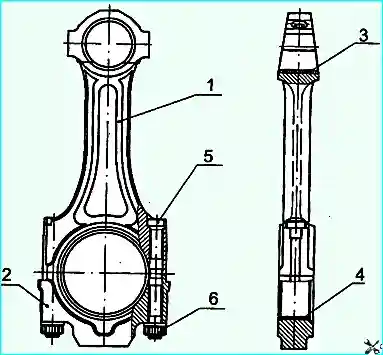
The connecting rod (Figure 2) is made of steel, forged, the shank 1 has an I-section. The connecting rod upper head is non-detachable, the lower one is made with a straight and flat joint.
The connecting rod is finally machined assembled with the cap 2, therefore the connecting rod caps are not interchangeable.
Into the connecting rod upper head, a steel-bronze bush 3 is pressed, and into the lower one, replaceable shells 4 are installed.
The connecting rod lower head cap is fastened by means of nuts 6, screwed onto the bolts 5 previously pressed into the connecting rod shank.
The connecting rod bolts are tightened according to the scheme defined in the article Tightening torques of the KAMAZ diesel fasteners.
On the cap and shank of the connecting rod, pairing marks are applied — three-digit ordinal numbers. In addition, on the connecting rod cap the ordinal number of the cylinder is stamped.
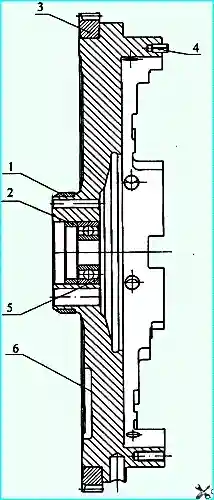
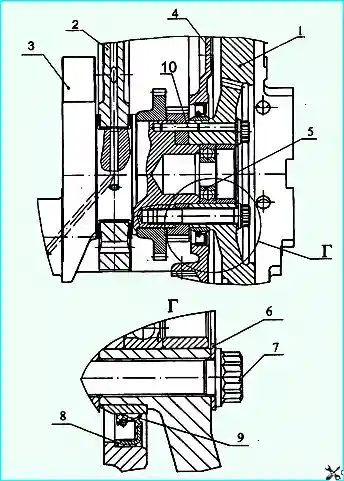
The flywheel (Figure 5) is fastened by ten bolts 7 (Figure 6), made of alloy steel, on the rear end face of the crankshaft and is fixed by the pin 10 (Figure 6) on the crankshaft centring journal 9 (Figure 3).
In order to exclude damage to the flywheel surface, a washer 6 (Figure 6) is installed under the bolt heads.
The value of the tightening torque of the flywheel fastening bolts is indicated in the article Tightening torques of the diesel fasteners.
On the machined cylindrical surface of the flywheel, a toothed rim 3 (Figure 5) is press-fitted, with which the starter gear engages when starting the engine.
Under the crankshaft oil seal, a ring 1 with an outer chrome-plated surface is installed.
The flywheel is made for a single- or two-disc diaphragm clutch.
Into the inner bore of the flywheel, the gearbox input shaft bearing 5 is installed.
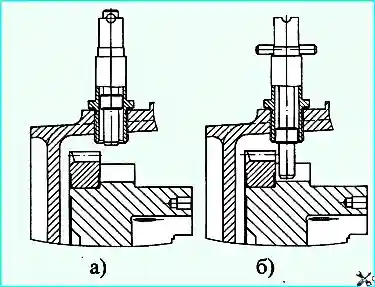
When adjusting the fuel injection advance angle and the thermal clearances in the valves, the flywheel is locked by a locking tool (Figure 7).
The flywheel construction has the following main differences from the flywheels of the 740.10 and 7403.10 engines:
- the angle of the groove for the locking tool on the outer surface of the flywheel has been changed;
- the diameter of the bore for accommodating the washer under the flywheel fastening bolts has been increased;
- a crescent-shaped recess has been introduced to ensure the required imbalance;
- the flywheel is fastened to the crankshaft end face by ten bolts M16×1.5.
The listed changes make it impossible to install flywheels of other engine models during repair work.
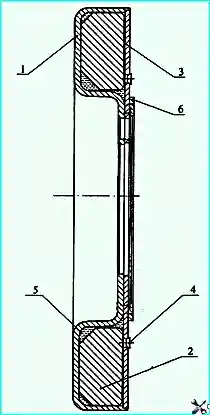
The torsional vibration damper (Figure 8) is fastened by eight bolts 2 (Figure 9) on the front crankshaft nose.
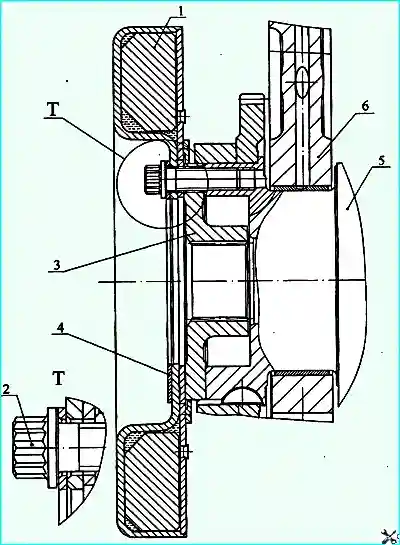
The damper consists of the housing 1 (Figure 8), in which the damper flywheel 5 is installed with a clearance. Outside, the damper housing is closed by the cover 2. The tightness is ensured by welding along the joint of the damper housing and the cover.
Between the damper housing and the damper flywheel there is a high-viscosity silicone fluid, dosed before welding the cover. The damper is centred by the washer 3 welded to the housing.
The damping of the crankshaft torsional vibrations occurs by braking the damper housing, fastened on the crankshaft nose, relative to the flywheel in the silicone fluid medium. In this case, the braking energy is released in the form of heat.
It is prohibited during repair work to deform the damper housing and cover. A damper with a deformed housing or cover is not suitable for further operation.
After installing the damper, check for the presence of a clearance between the damper and the counterweight.
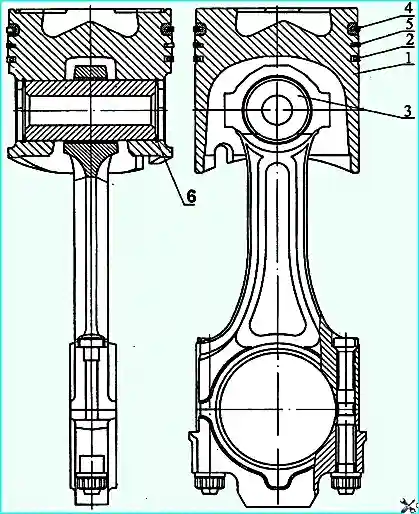
The piston 1 (Figure 10) is cast from aluminium alloy with an insert of wear-resistant cast iron under the upper compression ring.
In the piston crown, a toroidal combustion chamber with a displacer in the central part is made, which is displaced relative to the piston axis away from the valve recesses by 5 mm.
The lateral surface is a complex oval-barrel shape with a recess in the area of the holes for the piston pin. A graphite coating is applied to the skirt.
In the lower part of the piston skirt, a groove is made that, with correct assembly, excludes the contact of the piston with the cooling nozzle when it is at bottom dead centre.
The piston is complete with two compression rings and one oil scraper ring.
Its distinctive feature is the reduced distance from the crown to the lower end face of the upper groove, which is 17 mm.
On the engine, similarly to other models of KAMAZ engines, in order to ensure fuel economy and environmental performance, selective selection of pistons for each cylinder is used by the distance from the piston pin axis to the crown.
By the indicated parameter, the pistons are divided into four groups: 10, 20, 30 and 40. Each subsequent group differs from the previous one by 0.11 mm.
In spare parts, pistons of the greatest height are supplied — for the engines 740.50-360 and 740.51-320, the dimension from the piston pin axis to the piston crown of group 40 (the greatest) is 71.04-0.04 mm.
In order to avoid possible contact between them and the cylinder heads, in case of replacement, it is necessary to check the piston-to-head clearance.
If the clearance between the piston and the cylinder head after tightening the bolts of its fastening is less than 0.87 mm, it is necessary to trim the piston crown by the amount missing to this value.
The installation of pistons from KAMAZ engines of other models is not permissible. The marking of the piston 740.51-1004015 is made in casting on the inner cavity of the piston.
The compression rings (Figure 10) are made of high-strength cast iron, and the oil scraper ring — of grey cast iron.
The upper compression ring has the form of a two-sided trapezoid with an inner recess on the side of the upper end face, and the second has the form of a one-sided trapezoid.
During assembly, the end face marked "top" must be located on the side of the piston crown.
The working surface of the upper compression ring 4 is coated with molybdenum and has a barrel shape.
On the working surface of the second compression ring 5 and the oil scraper ring 2, chrome is applied.
Its shape on the second ring is a cone with a slope to the lower end face; by this characteristic feature the ring has received the name "minute ring".
Minute rings are used to reduce oil consumption by burning; their installation in the upper groove is not permissible.
The oil scraper ring is of the box type, 4 mm high, with a spring expander having a variable pitch of turns and a ground outer surface.
The middle part of the expander with a smaller pitch of turns, when installed on the piston, must be located in the lock of the ring.
The installation of piston rings from other models of KAMAZ engines can lead to an increase in oil consumption by burning and, as a consequence, to a deterioration in environmental performance.
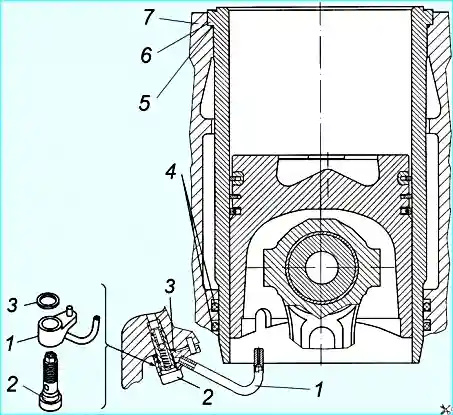
The cooling nozzles (Figure 11) are installed in the crankcase part of the cylinder block and ensure the supply of oil from the main oil line, when a pressure of 80–120 kPa (0.8–1.2 kgf/cm²) is reached in it, to the inner cavity of the pistons.
The valve located in each of the nozzles is adjusted to this pressure.
During engine assembly, it is necessary to check the correctness of the position of the nozzle tube relative to the cylinder liner and the piston. Contact with the piston is not permissible.
The piston is connected to the connecting rod (Figure 10) by a floating-type pin 3; its axial displacement is limited by retaining rings 6.
The pin is made of chrome-nickel steel, the hole diameter is 16 mm. The use of pins with a hole diameter of 22 and 25 mm is not permissible, since this disrupts the engine balancing.
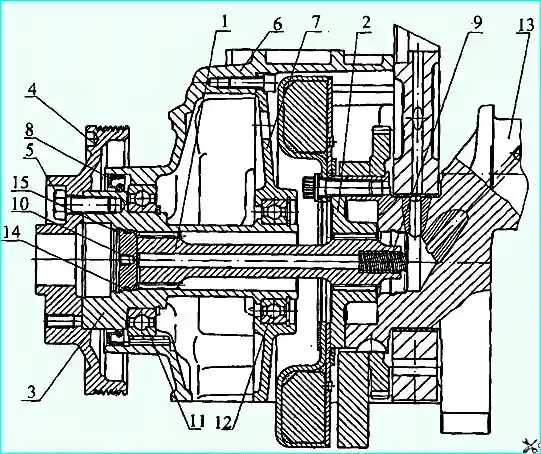
The front power take-off (Figure 11) is provided from the crankshaft nose through the power take-off half-coupling 2, fastened to the crankshaft nose 13 by eight special bolts M12×1.25.
The centring of the half-coupling relative to the crankshaft is carried out along the inner bore of the outboard counterweight.
The torque from the half-coupling is transmitted through the unit drive shaft 1 and the power take-off shaft 3 to the pulley 4.
The power take-off shaft 3 is installed on two ball bearings 11 and 12.
The sealing of the cavity is carried out by the oil seal 8 and the plug 10 with a rubber ring. To reduce the wear of the splined joints, the unit drive shaft is held against axial displacements by the spring 9.


