


The removal of the cylinder head from the engine was covered in the article “Cylinder head removal”.
The dismantling of the cylinder head is described in the article “Cylinder head dismantling”.
In this article we will cover the checking and repair of the cylinder head.
Preparation of the cylinder head for checking
We thoroughly wash the cylinder head and clean the oil galleries of the head. We remove carbon deposits from the combustion chambers and from the surface of the exhaust ports with a wire brush.
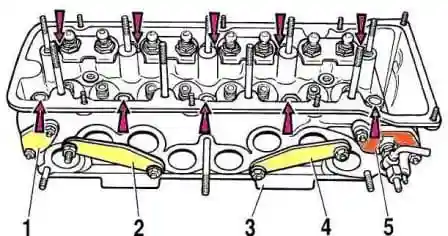
We inspect the cylinder head. Cracks anywhere on the head are not permitted. If there is a suspicion of coolant entering the lubrication system, the cylinder head must be checked for leaks.
To check for leaks, the openings of the cooling jacket of the cylinder head must be closed with plugs. There is a special set of plugs А.60334. But of course they can be made oneself from available materials.
Pump water into the cooling jacket of the cylinder head under a pressure of 0.5 MPa (5 kgf/cm²). Within two minutes no water leakage from the cylinder head must be observed.
The cylinder head can also be checked for leaks with compressed air; to do this, also fit the plugs of tool А.60334 to the cylinder head. Immerse the cylinder head in a bath of water heated to 60—80 °C and let it warm up for five minutes. Then supply compressed air into the interior of the head under a pressure of 0.15—0.2 MPa (1.5—2 kgf/cm²). Within 1—1.5 min no escape of air bubbles from the head must be observed.
Valve seats
The shape of the chamfers of the valve seats is shown in Figures 2 and 3.
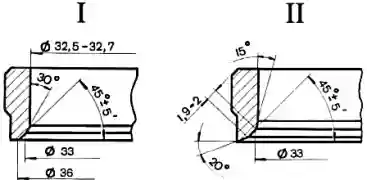
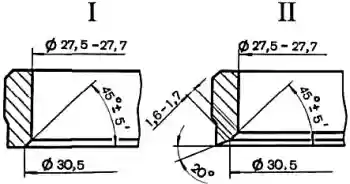
On the working chamfers of the seats (the contact zone with the valves) there must be no pitting, corrosion or damage. Small defects can be eliminated by grinding the seats, removing as little metal as possible. Grinding can be done both by hand and with a grinding machine.
To grind the seats, mount the cylinder head on a stand, insert drift А.94059 into the valve guide and clean the seat chamfers of carbon deposits with countersinks А.94031 and А.94092 for the exhaust valve seats and countersinks А.94003 and А.94101 for the inlet valve seats. The countersinks are fitted on spindle А.94058 and centred by guide drift А.94059. These drifts exist in two different diameters: А.94059/1 — for the inlet valve guides and А.94059/2 — for the exhaust valve guides.
Fit spring А.94069/5 onto guide drift А.94059, mount conical wheel А.94078 for the exhaust valve seats or wheel А.94100 for the inlet valve seats on spindle А.94069, secure the spindle in the grinding machine and grind the valve seat.
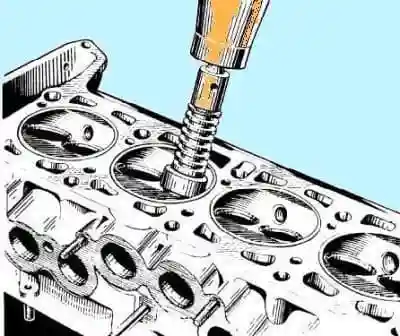
At the moment the wheel contacts the seat, the machine must be switched off, otherwise vibration will occur and the chamfer will be incorrect. It is recommended to dress the wheel with a diamond frequently.
For the exhaust valve seats, bring the width of the working chamfer to the values given in Figure 3 with countersink А.94031 (angle 20°) and countersink А.94092, which removes the work hardening on the inner diameter. The countersinks are fitted on spindle А.94058 and, just as when grinding, are centred by drift А.94059.
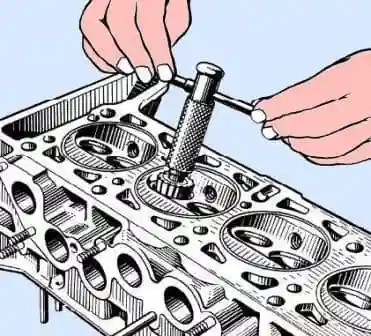
For the inlet valve seats, bring the width of the working chamfer to the values given in Figure 2, first machining the inner chamfer with countersink А.94003 (Figure 5) to a diameter of 33 mm, and then the 20° chamfer with countersink А.94101 to a working chamfer 1.9—2 mm wide.
Valves and valve guides
Remove carbon deposits from the valves. Check whether the stem is deformed and whether there are cracks on the valve head. Replace a damaged valve.
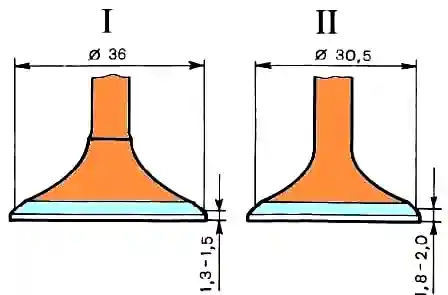
Check the condition of the working chamfer of the valve. In case of minor damage it can be ground, maintaining a chamfer angle of 45°30′±5′. The distances from the lower plane of the valve head to the base diameters (36 and 30.5 mm) must be within the limits given in Figure 6.
Check the clearance between the valve guides and the valve stem by measuring the valve stem diameter and the guide bore. The calculated clearance for new guides is: 0.022—0.055 mm for inlet valves and 0.029—0.062 mm for exhaust valves; the maximum permissible limit clearance (when worn) is 0.3 mm provided there is no increased noise of the valve train.
If the increased clearance between the guide and the valve cannot be eliminated by replacing the valve, replace the valve guides, using drift А.60153/R for pressing out and pressing in (Figure 7).
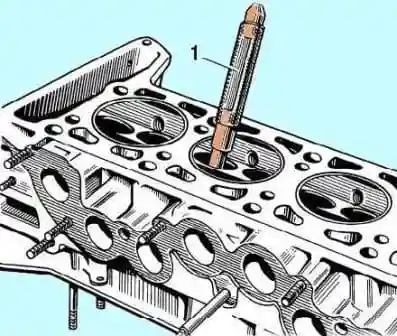
Press in the valve guides with the retaining ring fitted until it stops against the cylinder head body. After pressing in, ream the bores in the valve guides with reamers А.90310/1 (for inlet valve guides) and А.90310/2 (for exhaust valve guides).
Always replace the oil deflector caps of the valve guides with new ones when repairing the engine. Replace damaged oil deflector caps on the removed cylinder head. To press on the caps, use drift 41.7853.4016.
Springs
Make sure that the springs have no cracks and that their elasticity has not decreased; to do this, check their deformation under load (Figure 8).
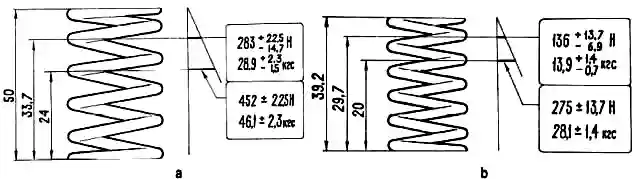
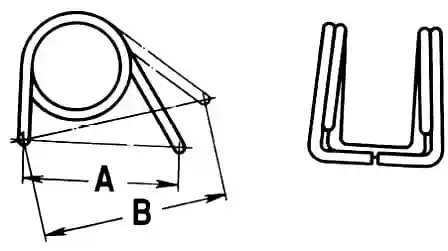
For the rocker springs (Figure 8), dimension А (spring in the free state) must be 35 mm, and dimension В under a load of 51-73.5 N (5.2-7.5 kgf) — 43 mm.
Cylinder head mounting bolts
With repeated use, the bolts stretch. Therefore check whether the length of the bolt shank (excluding the head length) exceeds 117 mm, and if it is greater, replace the bolt with a new one.
Valve rockers
Check the condition of the working surfaces of the rocker that are in contact with the valve stem, with the camshaft cam and with the spherical end of the adjusting bolt. If scoring or scores have appeared on these surfaces, replace the rocker with a new one. If deformation or other damage is found on the bush of the rocker adjusting bolt or on the bolt itself, replace the parts.


